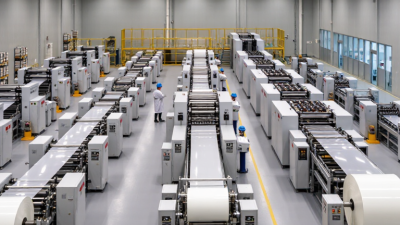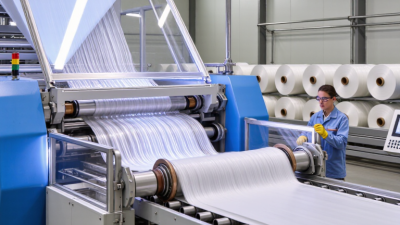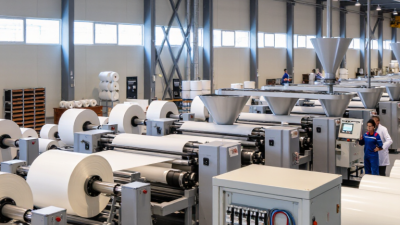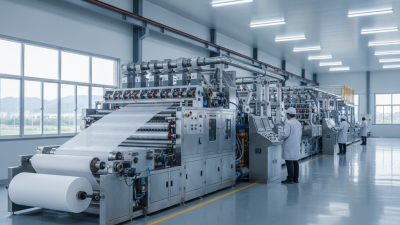
Choosing a Spunbond Non Woven Machine is a production decision, not merely an equipment purchase. The right line must match fabric weight, polymer type, output targets, energy limits, and future product plans. A machine that looks impressive on paper may perform poorly with unstable resin, uneven airflow, or limited technical support.
Industry data shows why this decision deserves careful review. Smithers projects the global nonwovens market to grow from approximately US$53.5 billion in 2023 to US$67.2 billion by 2028. Grand View Research also identifies strong growth in spunbond applications, including hygiene products, medical materials, agriculture, and construction. These figures suggest opportunity, but they do not guarantee profitability. Production speed alone can be misleading.
Dr. Seshadri Ramkumar, a widely recognized nonwovens expert, has said, “Nonwovens are everywhere in our daily lives.” That reality increases the need for consistent quality and responsible engineering. This guide examines die design, spinning technology, cooling systems, automation, energy consumption, maintenance access, and after-sales service. It also considers a less comfortable question: is the cheapest machine truly economical after downtime, waste, and operator training? Buyers should compare verified test data, not attractive brochures. Small details matter, such as web uniformity across the working width and the sound of a stable motor under continuous load.
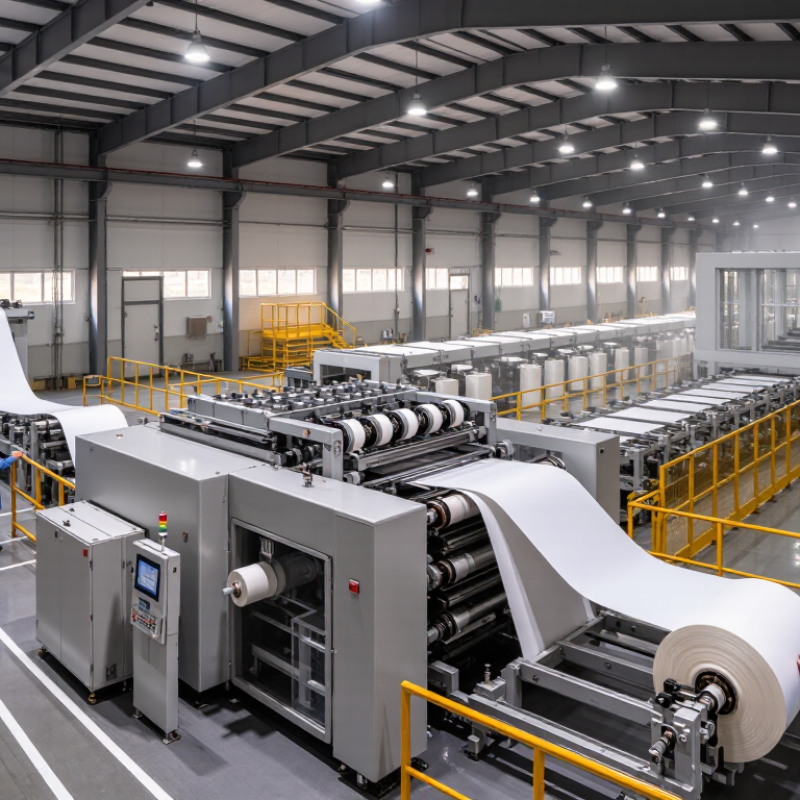
A spunbond non woven machine converts polymer resin into continuous filaments and forms them into a uniform fabric web. Typically, polypropylene or polyester pellets are melted in an extruder. The melt passes through spinnerets, while drawing air stretches the filaments. A conveyor then collects them evenly. Heat and pressure bond the web through a calender. The finished material may serve hygiene, medical, agriculture, construction, or packaging applications.
Machine choice should begin with product requirements, not advertised speed. Grand View Research estimates the global nonwoven fabric market reached about USD 53.5 billion in 2023, with continued growth expected through 2030. This expansion increases demand for stable, efficient production lines. However, market growth does not guarantee profit. A line with high output may create uneven weight, weak bonding, or excessive edge trim. Check working width, target GSM, polymer compatibility, line speed, energy use, and automatic quality controls. Smithers’ global nonwovens outlook also highlights hygiene and filtration as important growth areas, where consistency matters more than impressive maximum speed.
Tips: Request trial production using your actual resin and target GSM. Inspect filament uniformity, basis-weight variation, tensile strength, and power consumption. Ask for maintenance records and operator training details. Do not ignore factory space, cooling capacity, or spare-part access. A smaller line may fit your real market better. That point is easy to underestimate. Also, published capacity is usually theoretical. Test results deserve more trust than a brochure.
Choosing a spunbond non woven machine starts with clearly defining your production requirements. Decide the target fabric weight, roll width, daily output, and acceptable variation. A machine designed for 10–150 gsm fabric may not suit heavier technical materials. Specify whether you will process polypropylene, polyester, or other approved polymers. Each material affects temperature control, spinneret design, energy use, and maintenance needs.
Set measurable targets before comparing equipment. For example, define an output of 18 tonnes per day, a working width of 3.2 meters, and a GSM tolerance of ±2%. Also record your expected operating hours and product change frequency. Frequent changes require accessible components and simple cleaning procedures.
Check electrical load, compressed air demand, cooling water, floor strength, and ceiling height. These details are easy to overlook.
Quality requirements need equal attention.
Define tensile strength, elongation, uniformity, bonding strength, and roll hardness. Ask for test data from comparable production conditions, not only laboratory samples. A reliable supplier should explain control systems, spare parts, operator training, and service response times.
I have seen buyers focus heavily on speed, then struggle with unstable web formation. Speed is not everything.
Leave room for trial production and future product changes. Your first specification may be incomplete, and that is normal, but unclear targets create expensive compromises later.
Machine comparison should begin with your target fabric, not the equipment price. Grand View Research valued the global nonwoven fabric market at about USD 53.5 billion in 2023. This growth increases pressure on producers to improve consistency, speed, and energy control.
Compare spunbond, meltblown, and SMS configurations carefully. A spunbond line suits strong, breathable fabrics. Meltblown systems support finer filtration layers. SMS equipment combines both structures, but usually requires more complex process control.
Check working width, output per hour, basis-weight range, filament denier, and polymer compatibility.
A practical factory trial should measure GSM variation across the web, tensile strength, elongation, and roll hardness. These details often reveal more than a supplier’s brochure. Energy consumption matters too. Request data in kWh per kilogram at your expected production speed. Maximum speed can look impressive, but unstable production creates waste.
Tips: Compare complete-line performance, not isolated components. Ask for verified test records and recent operating data. Inspect automatic tension control, filter replacement time, die cleaning access, and changeover procedures. Shorter changeovers can protect margins. Still, automation is not always the best answer. Operators may need time to understand alarms and process drift. I would leave room for manual adjustment, because real production rarely behaves perfectly.
Machine quality begins with stable melt processing. The extruder should maintain accurate temperature control across every heating zone. Uneven heat can create thick spots, weak fibers, and frequent production stops. A well-designed spinning system also needs precise airflow and uniform die-hole distribution. These details directly affect fabric weight, strength, appearance, and waste levels.
Production efficiency depends on more than rated output. Check the machine’s real throughput under your target material and fabric specifications. Ask for trial data, energy consumption records, and continuous running results. Automatic tension control can reduce web breaks during winding. Quick-change components also shorten maintenance periods. Small delays become expensive over a full production month. Consistency matters.
Operators should inspect the control system, alarm records, and safety functions before purchase. Clear data displays help workers identify pressure, temperature, and speed changes quickly. Reliable machines should include accessible maintenance points and documented replacement procedures. Supplier training is equally important, especially during startup and troubleshooting. A machine may look impressive during a short demonstration, yet perform differently after several hours. This is easy to overlook.
Leave room for honest evaluation. Higher speed does not always mean better efficiency. Excessive speed may increase defects, energy use, and cleaning time. Compare useful fabric output, not only theoretical capacity. Request samples from extended trials, measure basis weight variation, and inspect edge quality. Independent testing can reveal problems that sales figures hide.
Choosing a spunbond non woven machine requires more than comparing catalog prices. Supplier evaluation should begin with operating evidence. Ask for production videos, recent customer references, and test reports showing output, GSM range, strength, and energy consumption. A factory visit can reveal practical details, such as material storage, assembly quality, and spare-parts organization. Do not rely on polished demonstrations alone.
Request a clear quotation with installation, training, freight, taxes, tooling, and commissioning listed separately. Calculate the cost per kilogram, not only the purchase price. Check expected waste, power demand, staffing, and maintenance intervals. A cheaper machine may become expensive when heaters, filters, or control components need frequent replacement. The numbers can be uncomfortable.
After-sales support deserves equal attention. Confirm warranty coverage, remote troubleshooting methods, response times, and spare-parts availability. Ask whether technicians provide installation records and operator training. A written service schedule is more reliable than a friendly promise. I once underestimated training time and lost several production days because operators misunderstood tension settings. That mistake changed how I assess suppliers.
Reliable suppliers should explain limitations honestly. Request a sample trial using your intended polymer and production settings. Compare the fabric’s uniformity, elongation, and defect rate across several hours. Keep every technical promise in the contract. Also check whether software updates, electrical diagrams, and maintenance manuals are included. Good support is measurable.
| Evaluation Dimension | Recommended Checkpoints | Typical Reference Data | Suggested Weight | Supplier Evidence to Request | Score Guide |
|---|---|---|---|---|---|
| Product Capacity | Compare rated output with the planned production volume, operating hours, and expected utilization rate. | Approximately 10–35 tonnes/day for many commercial spunbond lines; actual output depends on working width, product weight, polymer, and line configuration. | 15% | Signed technical specification, capacity calculation, production records from comparable installations, and a factory acceptance test plan. | 1–5 |
| Working Width | Check whether the usable width matches target products such as agricultural fabric, hygiene materials, packaging substrates, or construction membranes. | Common commercial configurations are roughly 1.6–5.2 m; wider lines are available for higher-volume production. | 8% | Layout drawing, usable-width tolerance, edge-trim arrangement, and finished-roll specifications. | 1–5 |
| Product Weight Range | Confirm stable production across the GSM range required by the business plan, including both light and heavy grades. | Many spunbond lines are designed for approximately 10–180 g/m², although the practical range varies by process and configuration. | 10% | GSM test results, sample rolls at different weights, thickness uniformity data, and process limitations. | 1–5 |
| Technology Configuration | Evaluate extruders, spinning beams, web-forming equipment, bonding system, winding unit, control system, and changeover design. | A single-beam line may be suitable for standard products; multi-beam configurations can support layered structures and broader product development. | 12% | Process-flow diagram, equipment list, component specifications, control architecture, and maintenance access drawings. | 1–5 |
| Energy Consumption | Compare total electrical demand, heating load, compressed-air use, and energy consumption per kilogram of finished fabric. | A reliable comparison should use measured kWh/kg at a stated GSM, polymer, line speed, and production rate rather than installed motor power alone. | 10% | Energy test protocol, guaranteed consumption range, motor-load list, heating specifications, and utility requirements. | 1–5 |
| Capital Cost | Separate the machine price from installation, utilities, building preparation, shipping, commissioning, spare parts, and operator training. | A complete commercial line can require a total project budget from several hundred thousand to several million US dollars, depending on capacity, width, automation, and scope. | 12% | Itemized quotation, exclusions list, payment schedule, delivery terms, installation scope, and tax or import assumptions. | 1–5 |
| Operating Cost | Calculate polymer consumption, electricity, labor, preventive maintenance, consumables, packaging, waste, and financing costs. | Use a five-year total-cost-of-ownership model; include planned downtime, start-up waste, trim waste, and replacement parts. | 10% | Cost-per-kilogram model, recommended staffing level, maintenance schedule, consumables list, and waste assumptions. | 1–5 |
| Quality and Process Stability | Assess GSM uniformity, tensile strength, elongation, appearance, roll hardness, winding quality, and startup repeatability. | Acceptance limits should be agreed before ordering; typical tests include GSM, tensile strength, elongation, thickness, air permeability, and visual inspection. | 12% | Sample-test reports, quality-control plan, calibration records, acceptance criteria, and warranty treatment for performance deviations. | 1–5 |
| Delivery and Installation | Review manufacturing lead time, shipping method, site requirements, installation responsibilities, commissioning, and ramp-up support. | Large production lines commonly require several months for engineering, fabrication, testing, shipment, installation, and commissioning. | 6% | Project schedule, milestone plan, site-readiness checklist, installation staffing plan, and commissioning procedure. | 1–5 |
| Warranty Coverage | Check warranty duration, covered components, exclusions, response time, labor coverage, and performance guarantees. | A 12-month warranty from installation or 18 months from shipment is commonly used in industrial equipment contracts; the exact terms must be written into the agreement. | 7% | Warranty certificate, guaranteed performance schedule, exclusions, claim process, and spare-parts responsibility. | 1–5 |
| After-Sales Service | Evaluate remote diagnostics, technical response time, local service capability, training, preventive maintenance, and emergency support. | A practical service target is a response within one business day for remote support, with critical spare-parts availability planned before commissioning. | 10% | Service-level agreement, support contacts, escalation procedure, technician availability, training program, and service-case references without relying on brand names. | 1–5 |
| Spare Parts Availability | Identify critical parts for extruders, heaters, sensors, drives, pumps, cutters, winders, and control systems. | Prepare an initial spare-parts package for commissioning and at least the first 12–24 months of operation, based on supplier recommendations. | 5% | Critical-parts list, prices, lead times, recommended stock levels, compatibility information, and parts obsolescence policy. | 1–5 |
| Supplier Verification | Verify manufacturing capability, engineering resources, quality systems, export experience, financial stability, and reference projects. | Request at least three comparable operating references and independently confirm production status, machine age, output, and service history. | 8% | Factory audit, production records, customer reference calls, inspection reports, certifications, and contract-fulfillment history. | 1–5 |
| Commercial and Contract Terms | Review payment milestones, inspection rights, liquidated damages, acceptance testing, delivery terms, dispute resolution, and documentation. | Link final payment to documented factory and site acceptance results rather than paying solely against shipment. | 5% | Draft contract, technical annex, acceptance protocol, packing list, manuals, drawings, software-backup policy, and training deliverables. | 1–5 |
Note: Cost ranges and technical figures are indicative industry reference values, not quotations. Final evaluation should be based on a comparable technical specification, written guarantees, tested samples, and a total-cost-of-ownership calculation.